The Duravant family of operating companies serve the food processing, packaging and material handling segments.








Rigid Modular and Live Roller Conveyors
FMH Conveyors provides rigid modular conveyors that help shipping, receiving, distribution, and fulfillment teams adjust package flow as operating needs change. Modular sections can be set up, moved, or reconfigured for changing processes.
This flexibility helps facilities make better use of floor space while keeping package movement efficient. Live roller conveyors can add powered movement where needed for transfers, sorting, and connected workstations.
Why Choose Rigid Modular Conveyors for Your Facility?
Rigid modular conveyors give operations a practical way to change layouts without treating the conveyor path as permanent. BestConnect modules can be rearranged as package flow, staffing, workstation locations, or facility needs change. That flexibility can reduce disruption during seasonal volume shifts or process updates. Less disruptions means your team can keep existing equipment in use longer.
Portable modular sections can also move between work areas when demand changes. By combining durable construction with a reconfigurable design, BestConnect helps facilities support growth while getting more value from their conveyor investment. BestConnect is a highly reconfigurable solution designed to adapt as business needs change.
BestConnect Live Roller and Modular Conveyor Options
FMH Conveyors offers BestConnect options for both powered package movement and flexible layout changes. BestConnect MDR uses motor-driven rollers for package transfers, semi-automated sorting, and connections to manual packaging or workstations. BestConnect Modular Conveyors use highly adaptable components that can be arranged as business requirements change.
Together, these options let facilities use live roller conveyors where powered movement is useful while keeping rigid modular conveyors at the center of the layout. Both are designed for quick installation or reconfiguration with minimal components and simple controls.
Configure Rigid Modular Conveyors Around Your Workflow
BestConnect components can be combined to guide products through the available space in a facility. Straight sections create the main path, while curves change direction. Centralizers help position packages, skews move products toward one side, and coated roller inclines can change elevation. Merges bring package lanes together, and lift gates can create operator access points.
These components help route products around equipment, connect work areas, and adjust conveyor flow as needs change. The modular design also supports faster installation and future reconfiguration.
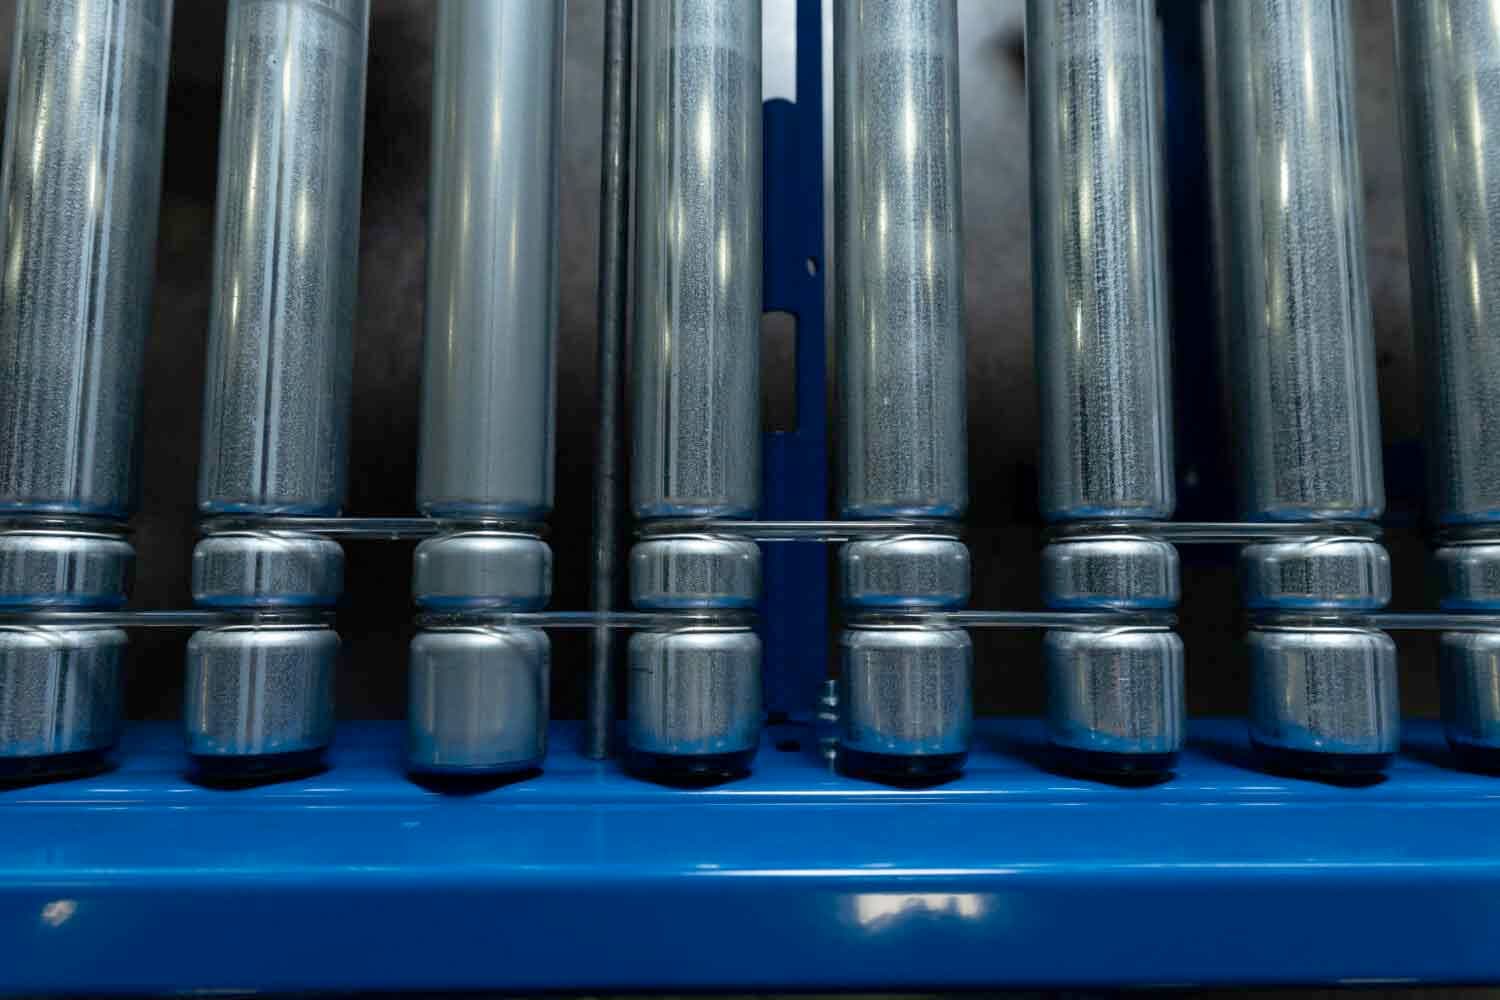
BestConnect MDR Conveyor
Our motor driven roller conveyors can be utilized to create systems for a variety of applications including package transfers, semi-automated sorts, and tying in manual packaging/workstations. These solutions can be quickly installed or reconfigured thanks to modular design, minimal components/hardware, and simple controls.
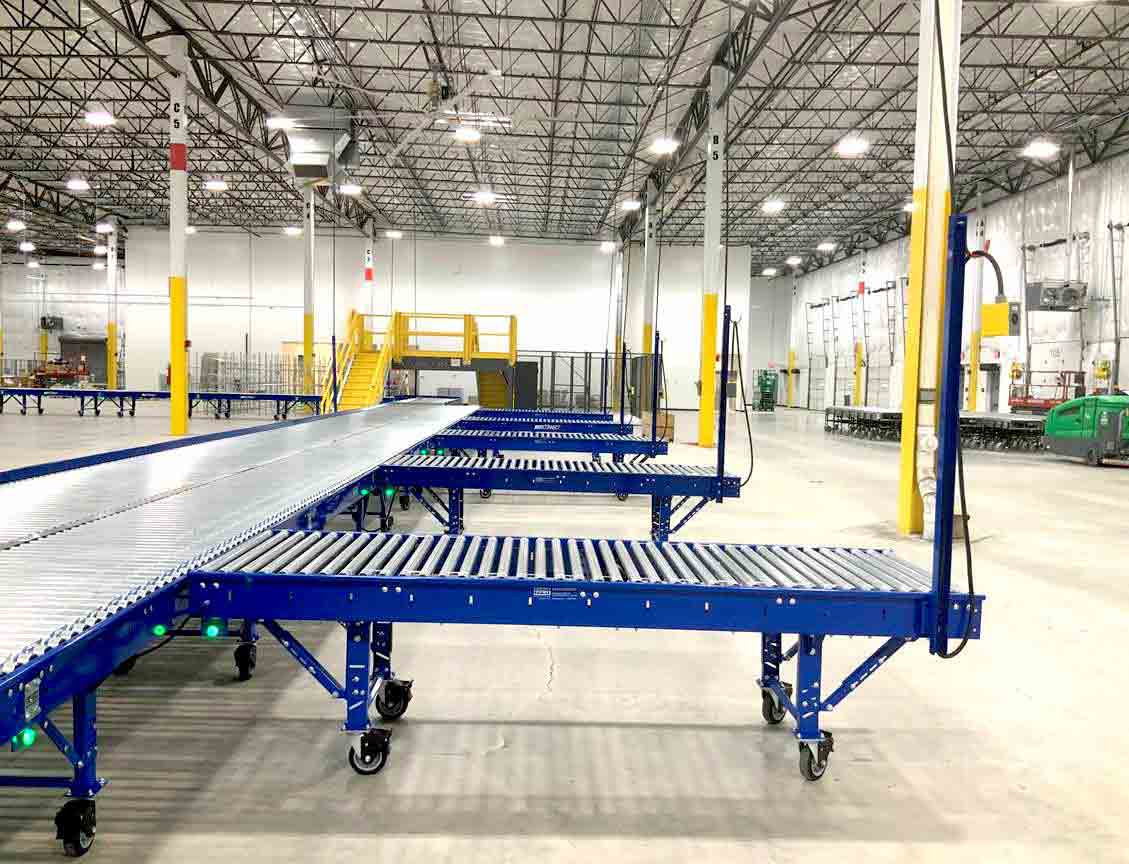
BestConnect Modular Conveyors
These conveyor modules provide a solution that allows companies to quickly adapt to changing business requirements by utilizing highly reconfigurable components.
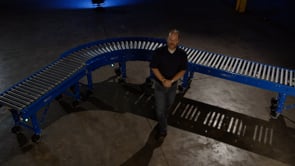
Advantages of a Modular Conveyor Design
A modular design can help teams respond faster when package flow or floor space changes. Fast configuration makes it easier to adapt. Minimal components can simplify installation, while portable modules can be moved between locations when needed.
This flexibility can streamline productivity when layouts change and can help facilities use available floor space more efficiently. When powered live roller movement is part of the solution, packages can move through key transfer points with less manual handling.
Designed for Your Unique Application
Rigid modular conveyors can support package transfers, semi-automated sorting, and manual packaging or workstation connections. The layout can be adjusted to fit product flow and the way each operation works.
BestConnect solutions are used in:


FMH Conveyors works with customers to identify the right configuration for the application. Each facility receives a practical solution around its workflow instead of relying on one standard layout.
Application Support, Installation and Ongoing Conveyor Service
FMH Conveyors supports customers beyond equipment selection. Our resources can help teams keep equipment aligned with changing operating needs while supporting uptime and long-term performance.
Our team works with yours to determine the best solution for your new belt-driven roller conveyor. On top of that, we offer installation support and integration with any existing conveyor system. For more information, Contact Us today or check out our blog.